
What Makes Mining Equipment Maintenance So Difficult?
Mining equipment maintenance is difficult because heavy assets run non-stop in harsh, remote conditions, spare parts are hard to stage, and records are often still on paper.
Maintaining a haul truck is nothing like maintaining a car. These machines work under constant stress, and the conditions work against every plan. Six challenges come up again and again:
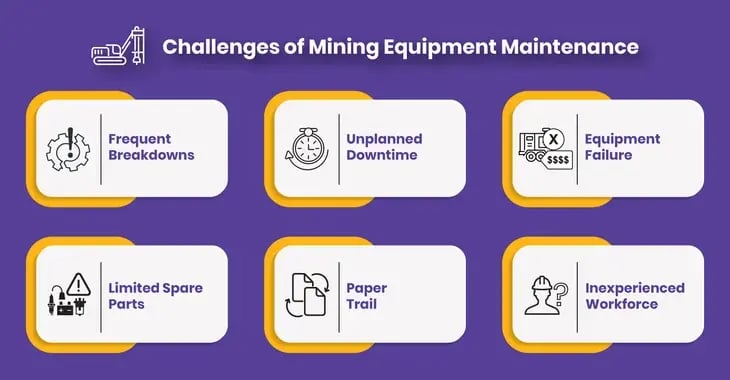
- Harsh operating conditions: Dust, extreme heat and cold, and constant vibration accelerate wear, so components fail faster than the manual predicts.
- Remote, distributed sites: Mines sit far from workshops and suppliers. Reaching a failed machine, and getting the right part to it, takes time most operations do not have.
- Aging, high-value fleets: Many mines run equipment well past its intended life. Older machines break down more often and need more attention to stay safe.
- Spare-parts availability: Long lead times and remote storerooms mean the part a repair needs is often not on the shelf when the machine goes down.
- Paper-based records: Maintenance history on paper is easy to lose and hard to analyze, so teams miss patterns and repeat the same failures.
- A shrinking skills base: Experienced technicians are retiring faster than they can be replaced, which puts pressure on both safety and quality.
None of these are new. What has changed is that mines now have practical ways to work around them.
How Much Does Poor Maintenance Cost a Mine?
Maintenance is an estimated 30 to 50 percent of a mine's total operating cost, and unplanned downtime is far more expensive than the same work done on a schedule.
Maintenance is one of the biggest cost lines a mine can control. Independent industry analyses put it at roughly 30 to 50 percent of total operating cost, and that share has been rising as fleets age.
The bigger cost is often hidden in downtime. On a large open-pit operation, lost production from a stopped line can run into millions of dollars a day. Remoteness makes it worse. When a critical part is not in the local store, it can take days to arrive, and the asset sits idle the whole time. A single driveline or gearbox failure on a haul truck can cost tens of thousands of dollars in lost production and emergency repair before the machine turns a wheel again.
The pattern behind most of this cost is reactive maintenance. Running equipment until it breaks costs far more than planned work, because it adds emergency freight, overtime, and the secondary damage a small failure causes when it is left to run.
From Reactive to AI-Guided Maintenance
This whitepaper maps the path from fixed intervals and paper records to AI-guided maintenance, and what it takes to get there.
Maintenance Strategies for Mining Equipment
The four main mining maintenance strategies are reactive, preventive, condition-based, and predictive. Most mines use a mix, matched to how critical each asset is.
|
Strategy |
How it works |
Best for |
|---|---|---|
|
Reactive (run to failure) |
Fix the machine after it breaks. |
Low-cost, non-critical assets with a spare on the shelf and no safety risk. |
|
Preventive (time or usage based) |
Service at set intervals or run hours. |
Assets with predictable, age-related wear, where the interval matches real failure data. |
|
Condition-based |
Trigger work from a measured signal such as vibration, temperature, or oil analysis. |
Assets that show a clear warning sign before they fail. |
|
Predictive |
Use continuous sensor data and models to forecast a failure before it happens. |
Critical, high-value assets where the lead time justifies the sensors and analysis. |
Most mines still lean on reactive maintenance for too many assets, which is the most expensive way to run a fleet. Moving critical machines to condition-based and predictive strategies is where the largest gains come from, because failures on big equipment almost always leave warning signs in the data for weeks before they happen.
The catch is that a strategy on paper saves nothing if the plan does not reach the technician on the haul road. That is a field-execution problem, not a strategy problem, and it is where digital tools make the difference.
Digital Transformation in Mining Maintenance
Digital transformation in mining maintenance means moving from paper and reactive work to connected, mobile, data-driven maintenance that reaches the technician at the machine.
Digitalization in mining often gets talked about as sensors and dashboards, but that is only half of it. Sensors can tell you a bearing is failing. They do nothing on their own to get the right technician, the right instructions, and the right part to the machine in time.
Real digital transformation closes that gap. It puts the work order, the equipment history, and the safety steps on a mobile device the technician carries to the asset, and it feeds what they find straight back into the system of record. In practice, that means:
- Frontline mobility: Technicians get work orders, digital work instructions, and asset history on a phone or tablet, even in areas with no signal.
- Clean data capture: What happens at the machine is recorded as it happens, with photos and readings, instead of on a sheet that gets keyed in later.
- A connected frontline: Operators, maintainers, and planners work from the same live picture, so a problem an operator spots on rounds becomes a work order without delay.
This is the core of what a connected worker platform does. It sits on top of the systems a mine already runs and turns the maintenance plan into work the field can actually complete.
Industrial AI in Action: The Rise of the Frontline Execution Platform
See how industrial AI is moving mining and heavy-asset work from paper and delay to real-time execution at the point of work.
Managing Spare Parts and Inventory in Mining
In mining, spare-parts availability decides how fast a repair finishes, so inventory accuracy is a core part of equipment maintenance, not a separate warehouse issue.
A maintenance plan is only as good as the parts behind it. In a remote mine, a missing component does not just delay a job. It can hold a critical asset down for days while the part ships in. That makes inventory management in mining a maintenance problem as much as a supply-chain one.
Two things drive parts readiness. The first is accurate inventory. If the system says a part is in stock and it is not, the technician arrives to an empty shelf and the repair stalls. The second is staging. The right parts need to be kitted and ready before the scheduled job, not found at the last minute.
Getting this right means mobile inventory and warehouse execution that keeps records accurate at the bin and links directly to the maintenance plan, so a work order and its parts move together.
Stop Losing Repair Time to an Empty Shelf
Accurate counts only pay off if the right parts are staged before the job starts. This guide shows how leading MRO warehouses kit and stage spare parts so technicians never wait on a part.
Best Practices for Mining Equipment Maintenance
- Match the strategy to the asset. Put critical machines on condition-based or predictive maintenance, and save run-to-failure for cheap, backed-up parts.
- Standardize inspections. Regular, structured operator rounds catch small problems early, before they become failures.
- Get the plan to the field. A work order stuck in the office helps no one. It has to reach the technician at the machine.
- Capture data at the source. Record work, readings, and photos at the asset, so the next decision is built on real history.
- Stage parts ahead of the job. Kit and confirm parts before the scheduled date, so repairs are not held up by an empty shelf.
- Close the loop with operators. The people running the machines see the first warning signs, so give them an easy way to raise them.
How Innovapptive Helps Mining Teams Maintain Equipment
Every challenge above comes down to the same gap: the distance between the maintenance plan in the system and the work that happens at the machine. When that gap is crossed on paper, time and data get lost. Innovapptive closes it.
Innovapptive's mobile maintenance software puts work orders, equipment history, digital work instructions, and safety steps on a device the technician carries to the asset. It works offline, which matters in a pit or underground where signal is unreliable, and it syncs automatically when the connection returns.
It runs on the broader connected worker platform, which links maintenance, operator rounds, and inventory on one system. That connection turns a warning sign on an operator's round into a scheduled work order with the right parts staged, rather than a note that gets lost. The platform supports the systems a mine already runs, including SAP and IBM Maximo, so it adds mobile execution without replacing the system of record.
For maintenance teams, that means:
- Fewer breakdowns, because inspections and condition data reach planners in time to act.
- Faster repairs, because technicians have the history, instructions, and parts they need at the machine.
- Better records, because clean data captured in the field feeds the next round of decisions.
See Mobile Maintenance in Action
Get the solution brief for a closer look at how Innovapptive digitizes maintenance execution for asset-heavy, remote operations.
What This Looks Like in an Asset-Heavy Operation
Discover How Indorama Rebuilt Maintenance Execution
Indorama Ventures closed the gap between its maintenance plan and its technicians. The results: backlog down 58 percent, parts availability up to 95 percent. See how they did it.
Unlock Margins Hidden in your Maintenance
Watch how leading manufacturers improve OEE, increase PM compliance, and reduce downtime through connected execution.
- 28-09-2026
Best Work Order Software: Top 9 Platforms Compared
Selecting the best work order software is a different decision for a large industrial plant than...
- 22-09-2026
Maintenance Troubleshooting: 5 Steps, Techniques & Tips
Maintenance troubleshooting is the work that stands between the moment an asset stops working and...
- 21-09-2026
Maintenance Latency: The Hidden Cost of Waiting in Plants
Your dashboards are green and every role is performing, yet the maintenance budget keeps climbing....